
Anonymous UK beverage manufacturer
HydraFMT alcohol recovery membrane system
A trial led membrane development project was scaled into a fully automated production system that met every design criterion, exceeded several performance targets and delivered a reported annual saving of more than £200,000.
Customer confidentialTrial to full scaleUK designed and manufactured
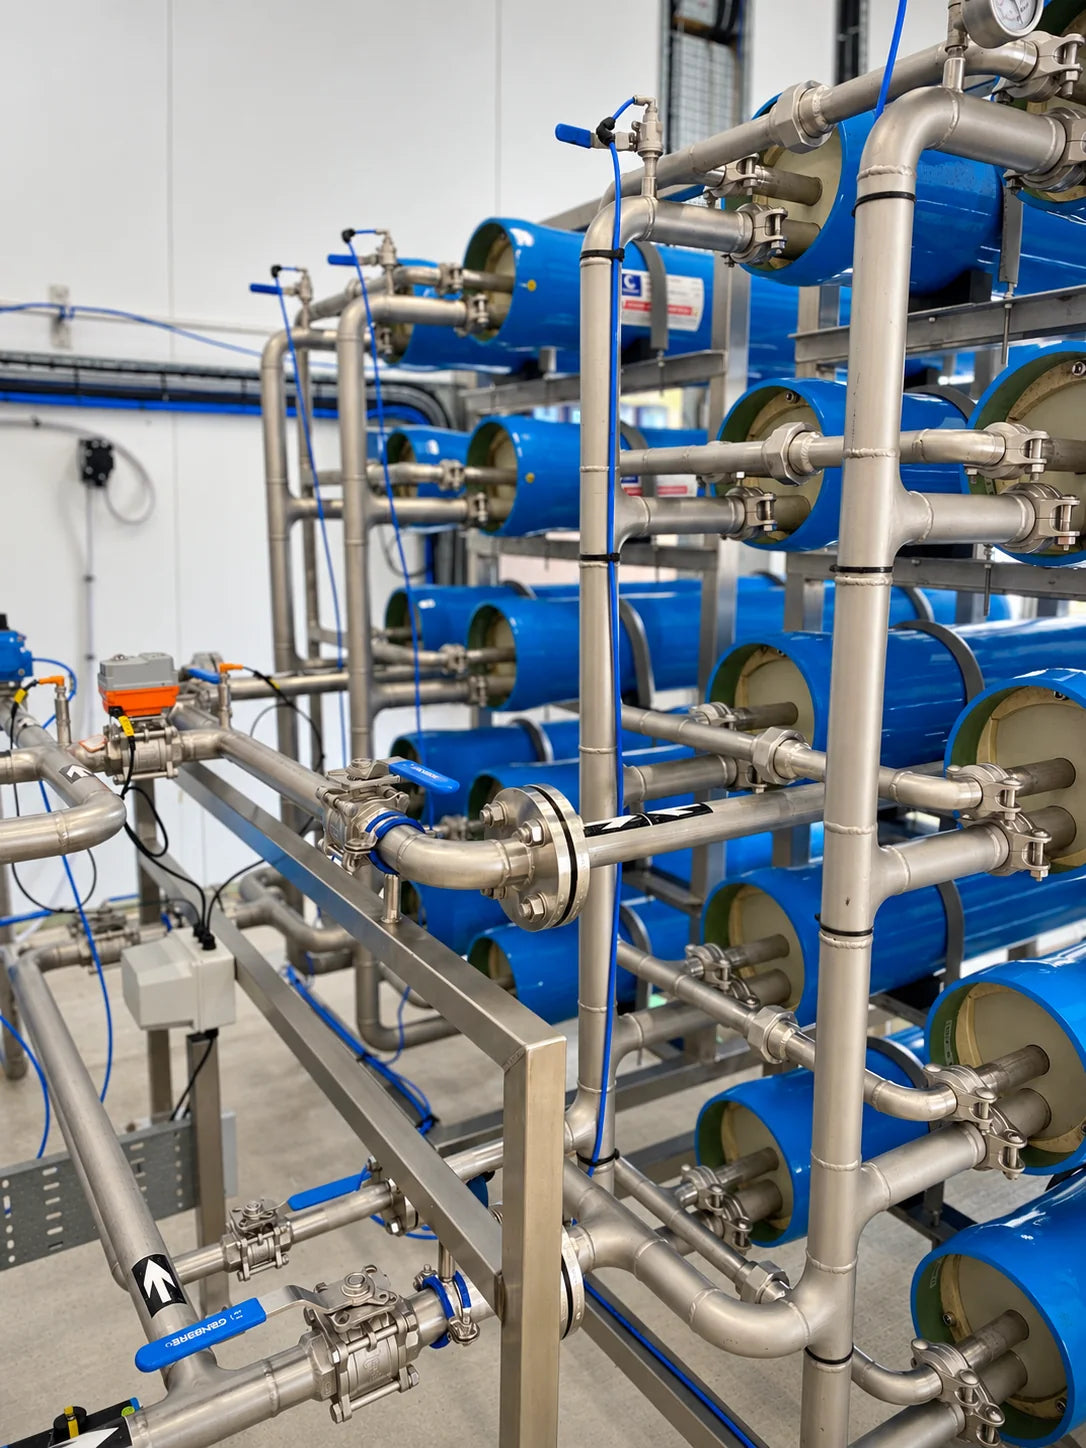
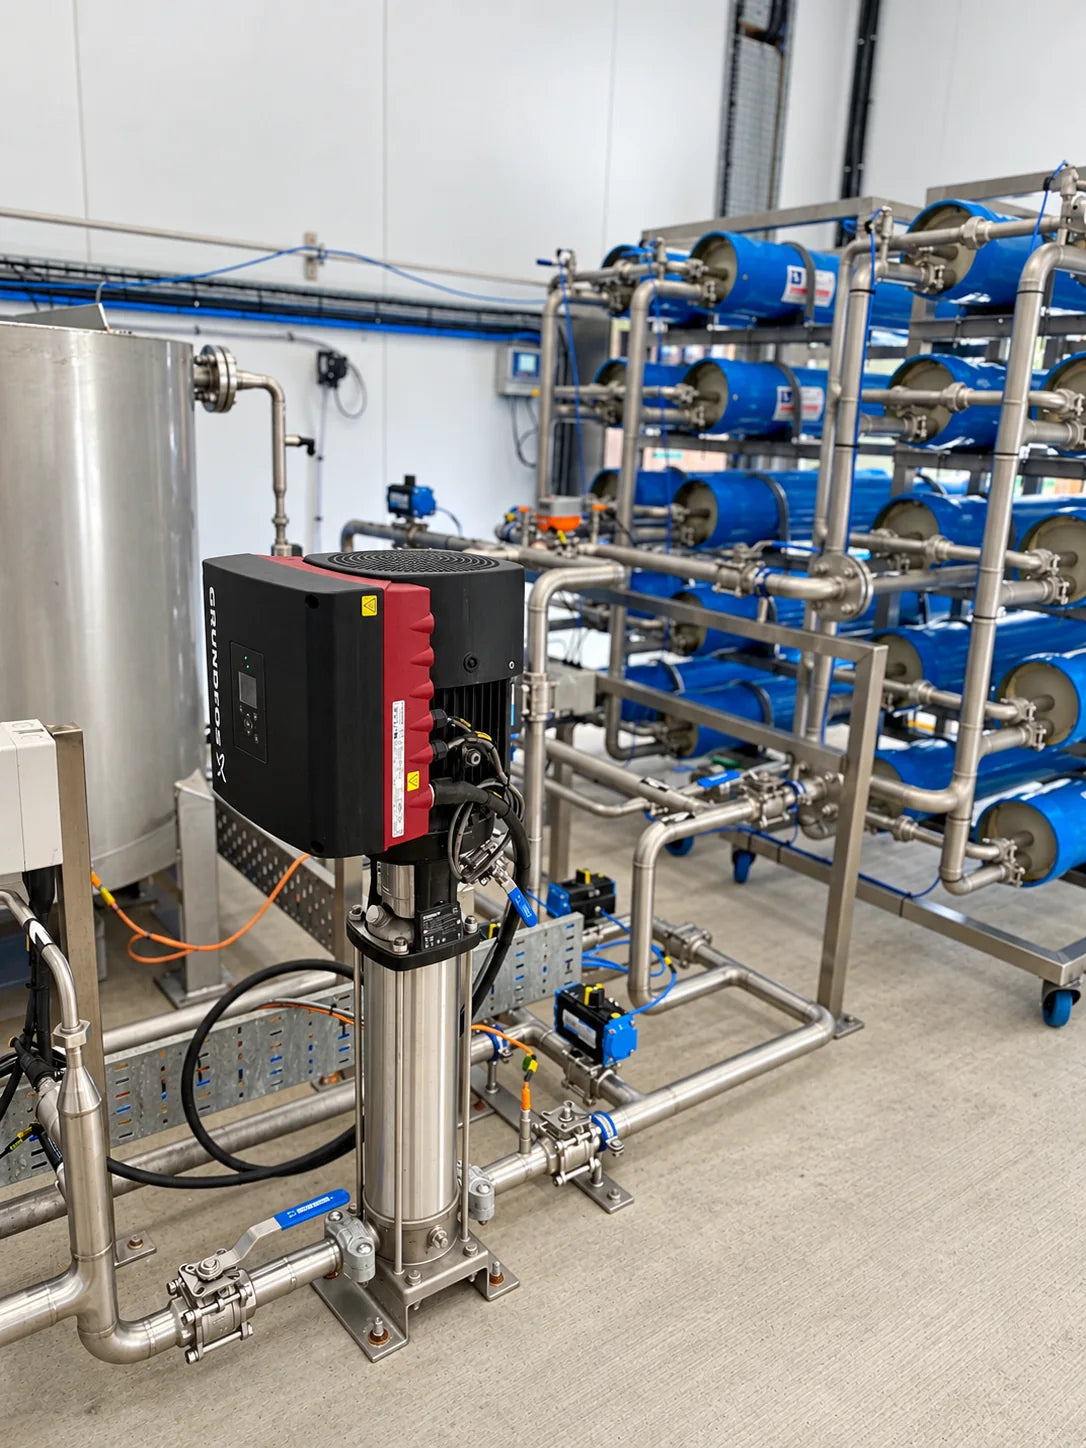
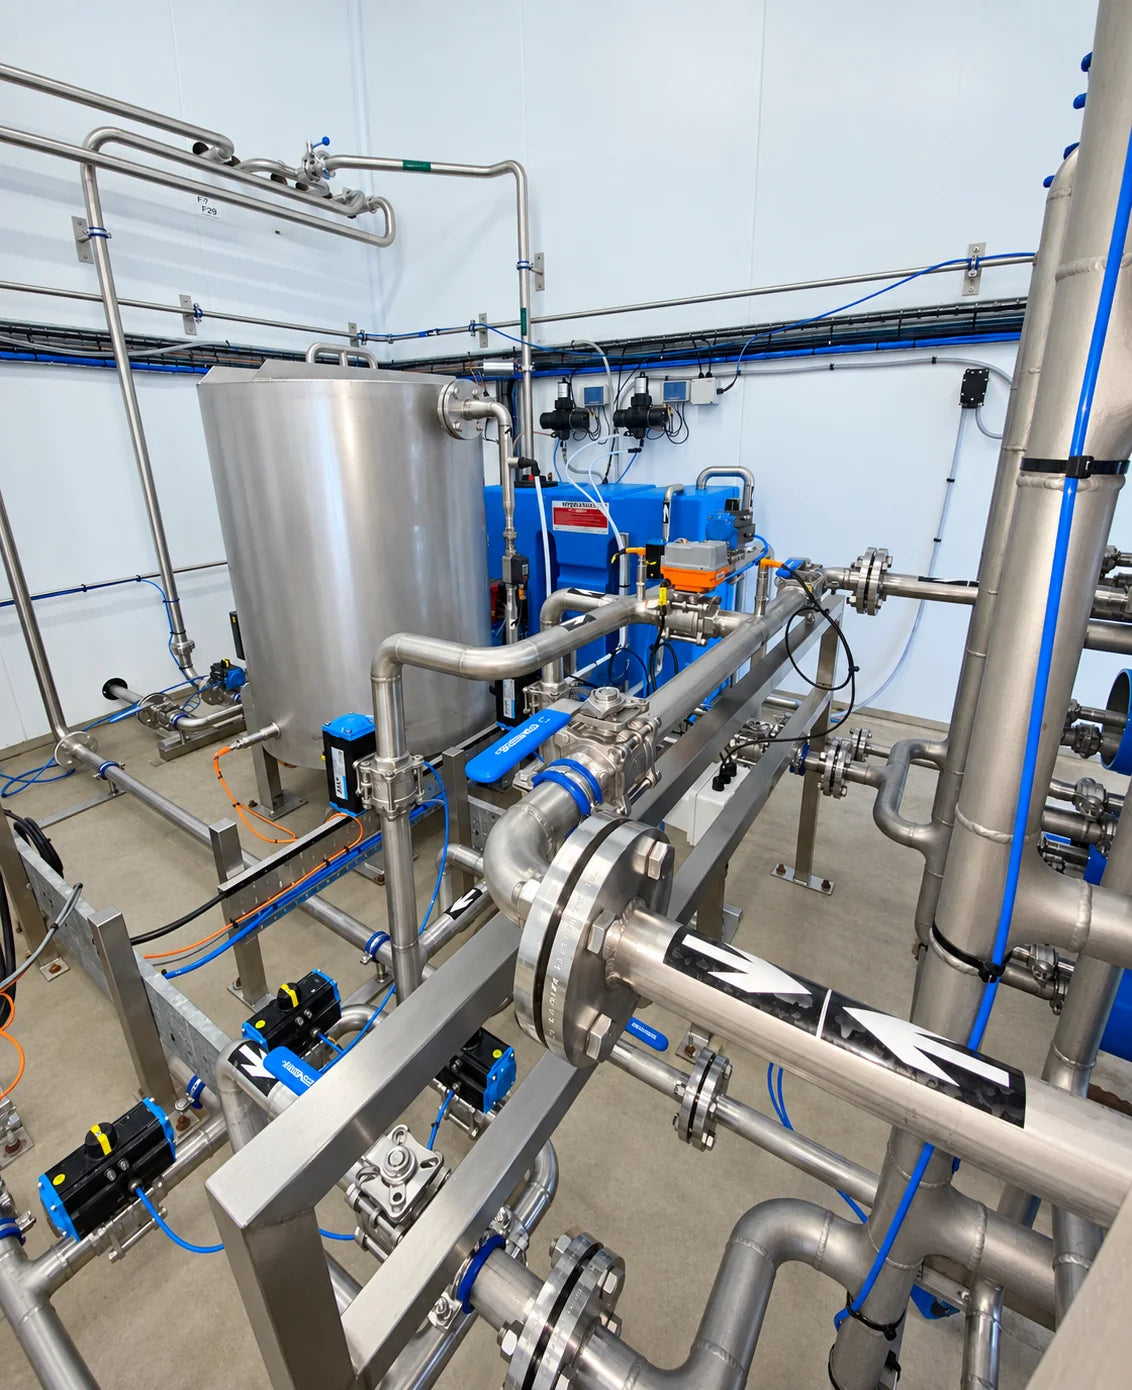
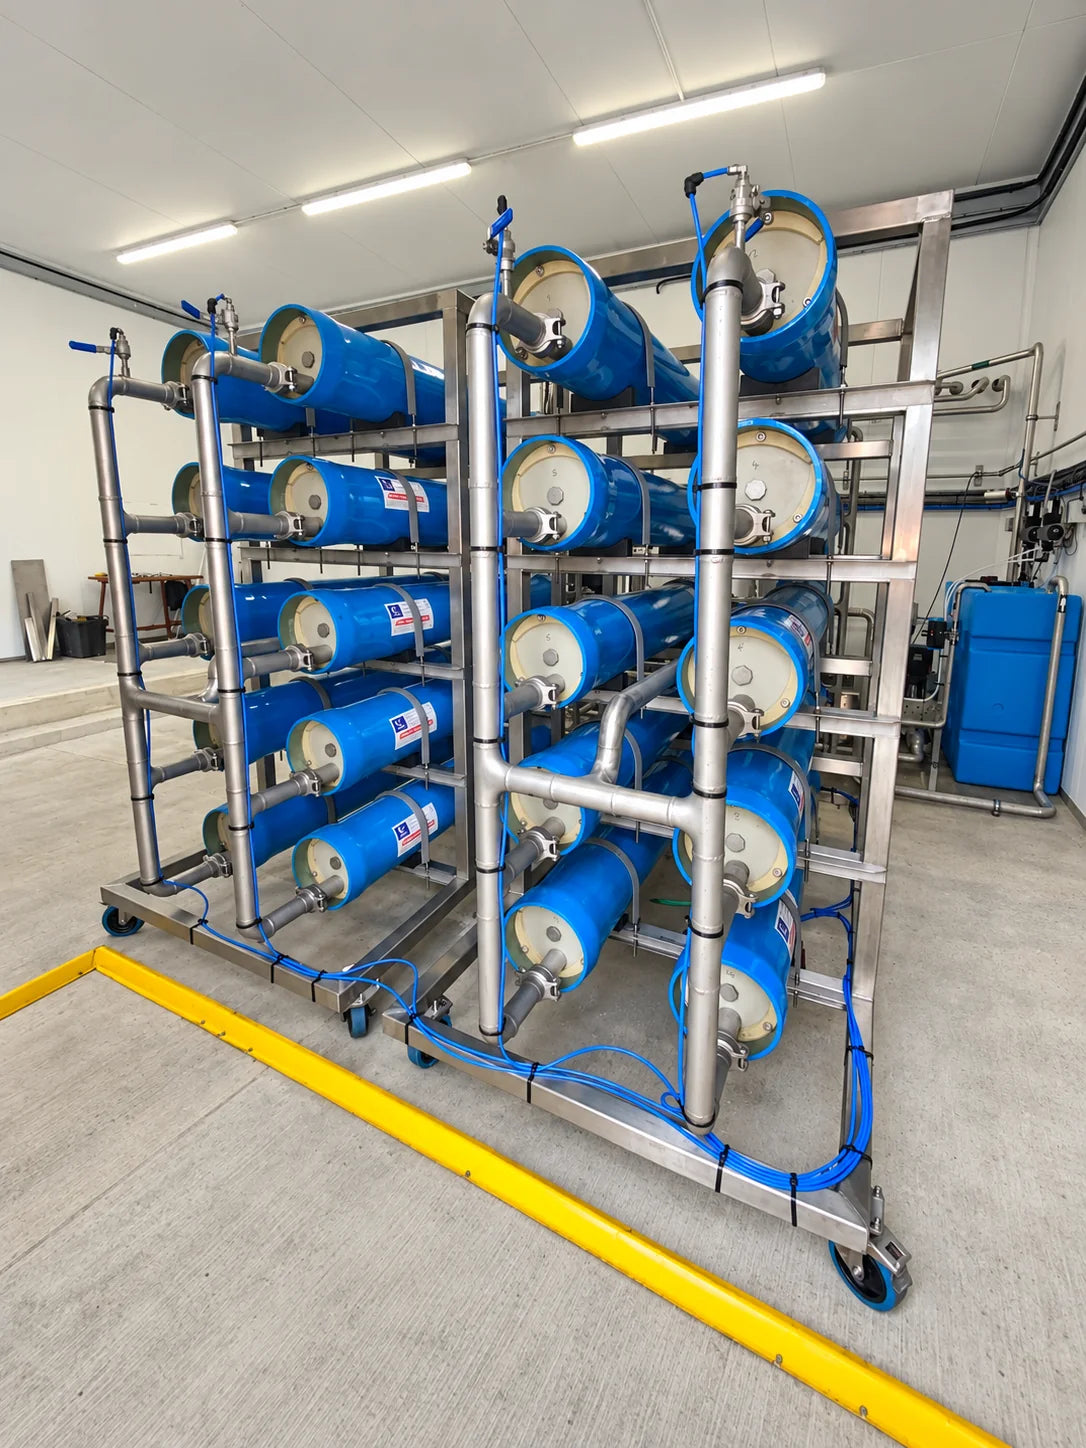
 Full scale HydraFMT system
The production problem
Recover the required alcohol fraction while improving product consistency.
The manufacturer needed to reduce unwanted colour, flavour and fermentation byproducts without losing the valuable alcohol fraction. The process also needed to operate consistently at production scale, integrate into the existing factory and provide a commercially stronger route than the previous method.
The customer name, formulation and detailed commercial inputs remain confidential. The performance and saving stated here were supplied by the customer following successful production operation.
Selective membrane separation rather than indiscriminate removal
Bench and pilot trials before full scale capital commitment
Automated production control and repeatable operating sequence
Designed around cleaning, operator access and maintainability
Quality improvement alongside a major operating cost reduction
Development route
Prove the separation, then scale the process.
The project was deliberately developed in stages. This reduced technical risk and allowed the full system to be engineered from measured performance rather than assumption.
01CharacteriseDefine the feed, contaminants, required alcohol recovery and product quality target.
02TrialTest membrane types and operating conditions against real production liquid.
03ConfirmMeasure separation, yield, cleaning response and repeatability.
04ScaleTranslate proven data into membrane area, hydraulics, controls and production capacity.
05CommissionOptimise the full system against the customer’s actual production process.
The engineered system
Purpose built equipment, not a laboratory rig enlarged by guesswork.
HydraFMT was engineered as a complete production package with membrane separation, process pumping, recirculation, instrumentation, automated sequencing and cleanable pipework integrated into one maintainable system.
Measured outcome
The commercial result followed the engineering result.
The completed system met the design criteria and exceeded performance expectations in several areas. The customer reported annual savings above £200,000 together with a better and more repeatable product.
Product qualityImproved control of unwanted colour, flavour and fermentation byproducts.
RecoveryValuable alcohol retained through a selective separation route.
ConsistencyAutomated operation reduced dependence on variable manual processing.
EconomicsReported annual saving exceeded £200,000.
Membrane trials and production scale up
Have a difficult liquid separation or recovery problem?
Hydra-Clear can assess the process, define a practical trial and use the results to develop a production scale system with a defensible performance basis.